A vibrating sieve separates material by giving particles repeated chances to find openings in a screen, but the nominal aperture never guarantees a perfectly sharp cutoff. By the end, you will know how to select the screen and settings, control the feed, prevent common failures, and verify the retained and passed fractions with test data.
Key takeaways
- Match screen aperture to the target particle-size range.
- Keep feed rate, moisture and distribution steady across the screen.
- Use deck arrangement to separate multiple size fractions efficiently.
- Verify results with representative samples from every outlet.
How vibration moves particles through the screen
Particles do not simply fall through a vibrating screen; they are repeatedly lifted, spread and presented to the apertures. This motion creates stratification: finer particles move toward the mesh, while larger particles travel across it toward the oversize outlet. That is the mechanism behind particle separation by size.
The useful force depends on both vibration frequency and stroke. For sinusoidal motion, peak acceleration is approximately a = (2πf)²A, where A is displacement amplitude. At 20 Hz and 3 mm amplitude, acceleration is about 4.8 g. Frequency has a squared effect, so a small speed increase can change conveying, contact time and separation sharply.
Confirm whether a supplier quotes stroke, amplitude or peak-to-peak displacement.
More acceleration can improve stratification, but excessive vibration makes particles bounce over the mesh, increases dust and noise, and carries near-size particles into the wrong fraction. A deep or uneven bed creates the same problem because lower-layer particles have fewer chances to reach the screen.
A nominal aperture is not an exact cutoff. A 1.0 mm opening does not guarantee that every particle below 1.0 mm passes, or that every larger particle is rejected. Near the opening, passage depends on particle shape and orientation, moisture or agglomeration, and residence time.
A vibrating sieve therefore performs probabilistic classification, not a perfectly sharp separation.
How to choose the aperture, screen area and deck arrangement
Choose the aperture from the required product distribution, then size the screen area for the feed load. A nominal mesh size identifies the cloth specification; its aperture size is the clear opening, and neither guarantees an exact product cutoff. Particles near that opening pass according to shape, orientation and residence time.
| Decision | Selection guide | Why it matters |
|---|---|---|
| Aperture | Choose an opening near the boundary between the fractions | A smaller aperture improves fines removal but reduces capacity and can increase blinding |
| Screen area | Increase area when feed rate rises or open area falls | Fine wire cloth provides less open area, so a physically large screen can still be the bottleneck |
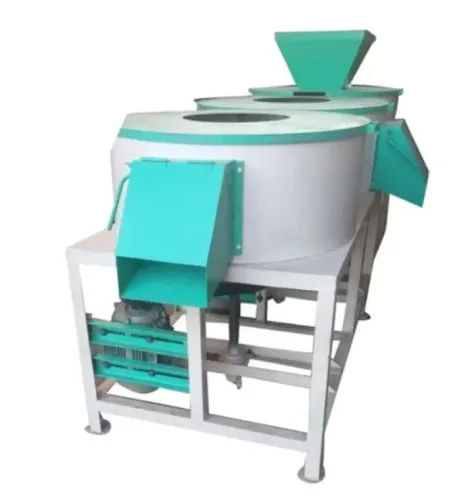
| Screen diameter | Select a diameter that provides the required usable area without overloading the discharge path | A larger screen diameter spreads the bed and gives near-size particles more opportunities to pass |
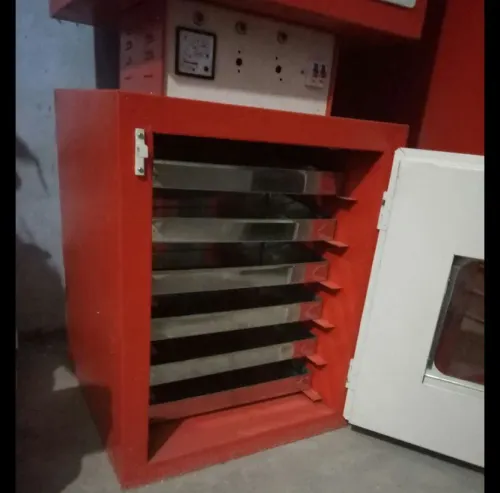
| Deck count | Use one deck for one cut; add decks for successive coarse-to-fine cuts | Put the coarsest cut on the upper deck and the finest cut below it, then check the most heavily loaded deck |
| Vibration | Start at the lowest acceleration that stratifies the bed and maintains movement | Excessive vibration causes bouncing, shorter contact time, dust, noise and near-size carryover |
Report the actual cut size from a test, not from the nominal mesh size alone. Specify the material, feed rate, moisture range, screen cloth, vibration setting, sample mass, sieve set and shaking time.
If the target is a particle-size distribution, compare measured fractions at those conditions; a 1.0 mm aperture is not proof that every particle below 1.0 mm will pass.
How feed conditions determine separation consistency
A steady feed produces a shallow, even material bed, giving near-size particles repeated chances to reach the cloth. A surge overloads the surface, traps fines beneath coarse particles and sends undersize material to the oversize discharge as carryover.
- Moisture and fat content: Surface moisture makes fines adhere to coarse particles or the cloth; higher moisture can form lumps. Fat creates sticky deposits that cause screen blinding and reduce open area. Control conditioning and check the material at the actual production moisture and temperature.
- Particle shape: Flat, fibrous or elongated particles can bridge apertures, while rounded particles pass more readily. Expect a less consistent cut when shape varies between batches.
- Density: Dense particles sink through a bed faster; low-density particles ride on top and can leave with the coarse fraction. Keep feed depth and vibration settings stable rather than compensating with speed alone.
- Agglomeration: A vibrating sieve classifies bonded lumps as oversize, not their individual primary particles. Use upstream de-lumping, milling or controlled conditioning when the product must be separated into primary particles.
Prevent pegging by selecting a suitable aperture and using screen cleaners such as bouncing balls or sliders where compatible with the product. Remove sticky deposits before they harden, and replace worn or loose cloth. Inspect seals and gaskets too: a bypass leak can put fines in the wrong discharge even when the screen is clean.
A practical operating sequence for stable screening
Begin with an empty, correctly tensioned screen and clear discharge paths. Confirm that the screen, clamps, gaskets and dust seals are secure, then check that the receiving containers can hold the expected output.
1. For loading and start-up, start the dust extraction and screening motor before opening the feed gate. Let the machine reach its normal vibration pattern, then introduce a small amount of material and check that it spreads across the full screen width.
2. Set hopper surge control before increasing throughput. Use a slide gate, screw feeder or vibratory feeder to maintain a shallow, even bed; a sudden dump creates carryover and overloads the screen.
3. Watch the feed zone and discharge continuously during the first few minutes. Screen bouncing, violent movement or material collecting at one edge indicates loose clamps, unbalanced loading, excessive amplitude or poor distribution. Correct the cause before raising the feed rate.
4. Adjust feed gradually while checking both fractions. Material discharge should remain steady, with no pulsing, bridging or dust plume; keep airflow controlled because aspiration can remove fines before they reach the undersize outlet.
5. For shutdown, close the feed gate and allow the screen to clear before stopping vibration. Stop extraction after airborne dust has settled, isolate power, empty the outlets and inspect the cloth for blinding, tears or trapped product. Clean before the next batch.
How to prove the separation result before approving a setup
Approve the setup only after it produces a measured mass balance at the intended production conditions. A dry, free-flowing trial can hide blinding, dust loss, agglomeration and poor near-size separation.
1. Define the test material and settings in writing: product lot, moisture content, particle shape, screen cloth, deck arrangement, feed rate, vibration setting and operating time. Use production material, or a closely matched substitute.
2. Weigh the feed charge before screening. Collect and weigh the retained and passed fractions separately, then record dust or material left inside the machine. The figures should reconcile within a preset tolerance; unexplained loss signals leakage, carryover or sampling error.
3. Take representative samples from each discharge. Perform sieve analysis with a named sieve set, sample mass, shaking time and reporting basis. Do not treat the nominal aperture as the product-size specification, because particle shape changes passage probability.
4. Set separate acceptance limits for passed-fraction recovery and retained-fraction contamination. A longer run or thinner bed can recover more undersize while sending acceptable product into the oversize stream, so one “efficiency” figure is not enough.
5. Repeat the checks during a run, including at start-up, steady state and near the end of the test. Repeat checks during a run expose moisture buildup, screen blinding and feed-rate drift.
If Unique Enterprises is evaluating a machine for you, require this test record with the screen specification and cleaning observations; in food or pharmaceutical service, also document contact-surface material, gasket condition, inspection access and contamination controls.
Related product
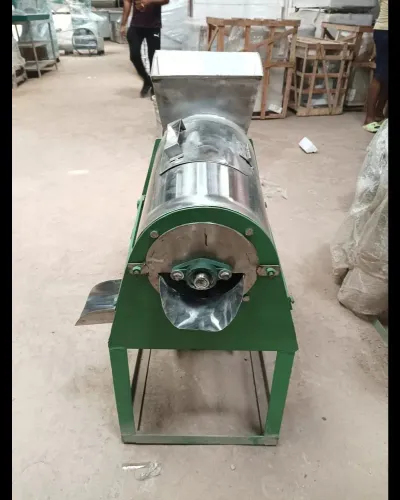
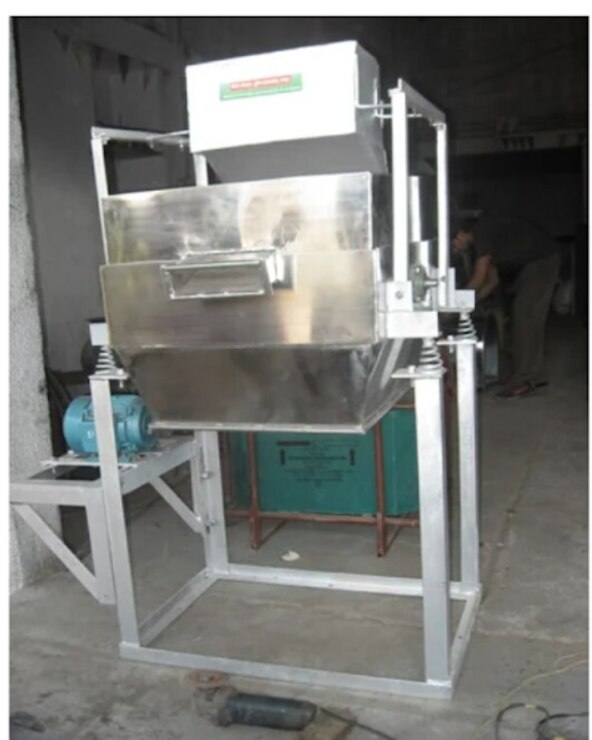
 | Vibrating Sieve Machine Product Details: Minimum Order Quantity 1 Unit Capacity 300 kg/hr Brand Unique Enterprises Automation Grade Semi-Automatic Material SS Voltage 230 V... View product → |
Frequently asked questions
How does vibration move particles through a sieve screen?
Vibration lifts and spreads particles, creating stratification that brings finer material toward the apertures while larger particles move toward the oversize outlet.
How do you choose the aperture, screen area and deck arrangement?
Choose the aperture for the target size cut, provide enough screen area for the feed load, and add decks when you need multiple size fractions.
Which feed conditions affect separation consistency?
Feed rate, moisture, particle-size distribution and even loading across the screen affect separation consistency.
How can you prove the separation result before approving a setup?
Collect representative samples from each outlet, measure particle-size results and compare them with the required specification before approving the setup.